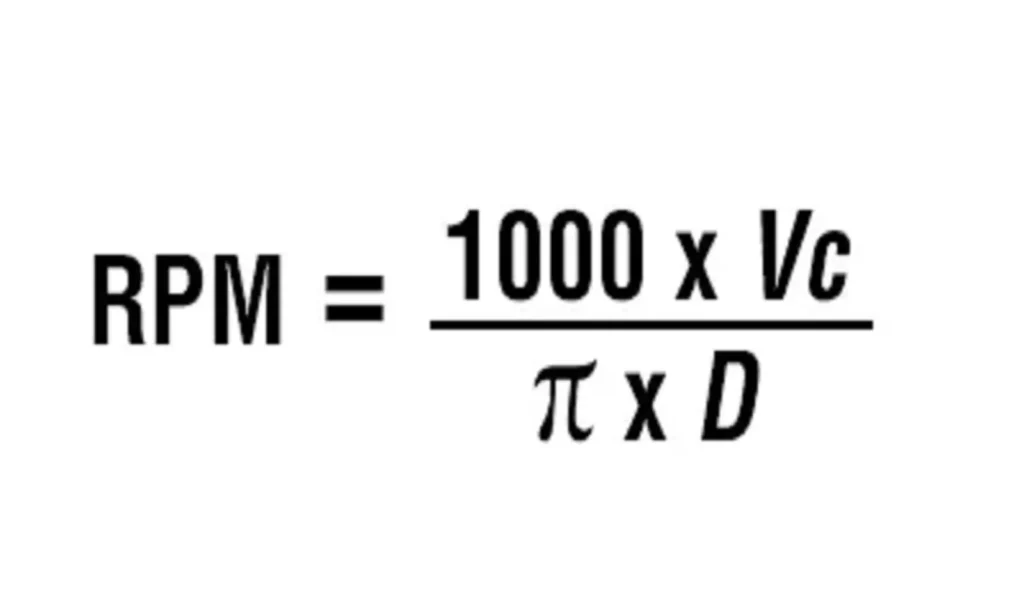CBN Inserts for Hardened 1045 Steel: Surface Finish, Tool Life and Cutting Parameters
Can you machine AISI 1045 steel with CBN inserts?
Yes—but whether CBN is the right choice depends much more on the hardness and condition of the workpiece than on the material name itself.
For annealed, normalized, or relatively soft 1045 steel, carbide is usually the more economical choice. Once 1045 has been induction hardened, flame hardened, or otherwise heat treated into the hard-turning range, PCBN can become a much better option, especially when the goal is stable dimensions, fine surface finish, and longer tool life.
This is the first rule to remember:
Do not choose CBN simply because the material is 1045 steel. Check the hardness first.
In this article, we use “CBN insert” because that is the common shop-floor term. More precisely, most CBN inserts used for hard turning are PCBN—polycrystalline cubic boron nitride cutting tools.
Can You Use CBN on AISI 1045 Steel?
AISI 1045 is a medium-carbon steel widely used for shafts, axles, pins, gears, sleeves, and other machine components.
C45, S45C, and Chinese 45 steel are often cross-referenced with AISI 1045 in industrial practice, although they should not automatically be treated as chemically identical under every material standard.
For cutting-tool selection, however, the more important question is often not whether the part is called AISI 1045, C45, or 45 steel.
It is:
What condition is the steel in now?
The same nominal steel grade may be machined in a relatively soft condition or after hardening to well above 50 HRC. The appropriate cutting tool can be completely different.
A practical starting point is:
| Workpiece condition | Typical tooling approach |
|---|---|
| Annealed or normalized 1045 | Carbide is normally the first choice |
| Moderately hardened 1045 | Compare carbide and PCBN based on hardness, tolerance, and production volume |
| Approximately 45 HRC and above | PCBN becomes increasingly attractive |
| 50–60+ HRC finishing | PCBN is often a strong choice |
| Severe interrupted cutting | PCBN grade and edge preparation must be selected carefully |
Commercial PCBN grades are commonly designed specifically for hardened steels. For example, Kennametal positions its KB1610 low-CBN-content PCBN grade for precision finishing of hardened steels above 45 HRC and explicitly advises against using that grade on soft steel.
Sandvik uses a more conservative broad definition of hard-part turning, describing it as the turning of hardened steels around 55 HRC and above, normally in finishing or semi-finishing operations.
The exact transition point therefore depends on the application, but the principle is clear:
As 1045 becomes harder, the case for PCBN becomes stronger.
Why PCBN Works Well on Hardened 1045 Steel
Hard turning puts a cutting edge under severe mechanical and thermal load.
PCBN is suitable for this environment because it combines very high hardness with strong wear resistance and the ability to retain cutting performance at elevated cutting temperatures.
This allows PCBN to maintain its cutting-edge geometry in situations where carbide wear may accelerate rapidly.
For production machining, that can mean:
- more stable dimensions;
- more consistent surface finish;
- fewer insert changes;
- less offset correction;
- and, in suitable applications, lower cost per finished part.
However, not all PCBN grades are the same.
Some grades are optimized primarily for wear resistance and high-speed continuous finishing. Others are designed with greater fracture resistance for interrupted cutting.
Sumitomo, for example, separates its hardened-steel CBN grades according to the application. Its BNC2105 grade emphasizes high-speed finishing, BNC2115 emphasizes high-precision machining and stable surface roughness, while BNC2135 is designed for higher fracture resistance in interrupted turning.
So choosing a CBN insert is not simply a question of choosing “the hardest insert.”
It is a question of balancing wear resistance, toughness, edge preparation, and the type of cut.
What Surface Finish Can CBN Achieve on Hardened 1045 Steel?
This is one of the most common questions in hard turning.
Under a stable finishing setup, sub-micron Ra is achievable with PCBN.
As a practical shop-floor reference, Ra 0.4–0.8 μm can be a reasonable target range for many optimized hard-turning applications. This is not a guaranteed value for every machine and every part.
The actual surface finish depends on much more than the insert material.
PCBN hard-turning research on other hardened steels has demonstrated surface roughness well below Ra 1 μm, including reported results as low as approximately Ra 0.25 μm under suitable conditions.
The important question therefore is not:
“Can CBN produce Ra 0.4?”
A better question is:
“Can my complete machining system hold the required Ra consistently throughout the tool life?”
Four factors are especially important.
1. Feed Rate
Feed is one of the first variables to examine when surface roughness is too high.
As feed increases, the geometric feed marks on the turned surface normally become more pronounced. Multiple hard-turning studies identify feed as one of the important factors affecting surface roughness.
This is why changing the CBN grade is not always the correct first response to a poor finish.
Sometimes the real problem is simply an unsuitable feed rate.
2. Nose Radius and Wiper Geometry
Tool geometry also has a major effect on the generated surface.
A suitable nose radius can improve finish, while a properly applied wiper geometry can allow a better surface finish at a productive feed rate.
Research on PCBN wiper inserts in hardened steel has shown significantly improved surface roughness compared with conventional geometry under the tested conditions.
But a larger nose radius is not automatically better.
Increasing the effective radius can increase radial cutting force. On a slender workpiece or an unstable machine, that may create chatter and actually make the finish worse.
3. Machine and Workpiece Rigidity
CBN cannot compensate for an unstable setup.
Typical problems include:
- excessive workpiece overhang;
- insufficient clamping;
- poor toolholder rigidity;
- spindle or bearing condition;
- excessive runout;
- and an unstable boring-bar setup.
The closer the surface-finish requirement moves toward Ra 0.4 μm or below, the more important the complete machine-workpiece-tool system becomes.
4. Tool Wear
A PCBN insert may still be physically cutting long after it has stopped producing acceptable parts.
Flank wear, notch wear, or micro-chipping can alter the effective cutting geometry and gradually increase surface roughness or dimensional drift.
In finish hard turning, this means useful tool life should often be defined as:
The point at which the tool can no longer maintain the required dimension or surface finish.
—not simply the point at which the cutting edge finally breaks.
How Much Longer Does CBN Last Than Carbide?
Customers often ask whether CBN lasts 5 times, 10 times, or even 20 times longer than carbide.
There is no universal multiplier.
In the right hard-turning application, PCBN may provide a very large increase in usable tool life compared with carbide. In another application, the difference may be much smaller.
The result depends on:
- workpiece hardness;
- microstructure;
- cutting speed;
- feed;
- depth of cut;
- continuous or interrupted cutting;
- PCBN grade;
- CBN content;
- edge preparation;
- coolant strategy;
- machine stability;
- and the tool-life criterion.
PCBN has demonstrated strong tool-life performance in hardened-steel turning, and comparative research has found PCBN capable of the longest tool life among tested cutting materials in some hard-turning conditions.
But a statement such as:
“CBN always lasts 10–20 times longer than carbide”
is too broad unless the machining conditions are also provided.
A useful comparison should look like this:
| Item | Carbide | PCBN |
|---|---|---|
| Parts per cutting edge | Actual measured result | Actual measured result |
| Cutting speed | Recorded | Recorded |
| Cycle time | Recorded | Recorded |
| Average surface finish | Recorded | Recorded |
| Dimensional corrections | Recorded | Recorded |
| Tool changes per shift | Recorded | Recorded |
| Tool cost per finished part | Calculated | Calculated |
If carbide produces 30 acceptable parts and PCBN produces 300 under comparable production conditions, then saying that PCBN delivered approximately 10 times the useful tool life is meaningful.
Without that application data, it is only a marketing number.
Recommended Starting Parameters for Continuous CBN Turning of Hardened Steel
Based on our practical application experience, the following range is a useful starting window for continuous turning of hardened steel with CBN/PCBN:
| Cutting parameter | Recommended starting range |
|---|---|
| Cutting speed, Vc | 120–180 m/min |
| Feed, f | 0.10–0.12 mm/rev |
| Depth of cut, ap | 0.10–0.30 mm |
| Application | Continuous turning of hardened steel |
These numbers should be treated as starting parameters, not universal fixed settings.
Our normal recommendation is:
Start at the lower end of the parameter range. Confirm cutting-edge stability, surface finish, and dimensional consistency first. If everything is stable, increase cutting speed step by step.
This approach is especially useful when the customer is trying PCBN for the first time or when the actual heat-treatment condition and machining stability are not yet fully known.
The appropriate final speed also depends on the specific CBN grade. Current Kennametal application data, for example, lists different speed ranges according to both PCBN grade and material hardness. For hardened materials in the 55–60 HRC range, the published ranges for two grades differ significantly, illustrating why grade-specific recommendations should always be considered.
Real Customer Example: PCBN Turning at HRC 58–60
Here is one actual customer machining condition from the field:
| Item | Customer condition |
|---|---|
| Workpiece hardness | HRC 58–60 |
| Cutting speed | 120 m/min |
| Depth of cut | 0.08–0.10 mm |
| Workpiece diameter | 100 mm |
| Workpiece length | 40 mm |
| Spindle speed | 380 rpm |
This is a useful example of a conservative finishing approach on a high-hardness workpiece.
The customer is running at the lower end of our normal 120–180 m/min cutting-speed window and using a relatively light depth of cut.
That is often a sensible strategy when:
- the workpiece is close to 60 HRC;
- surface finish is important;
- edge stability is more important than maximum metal-removal rate;
- or the application is still being optimized.
Notice also that the actual depth of cut, 0.08–0.10 mm, is slightly lighter than our general starting recommendation of 0.10–0.30 mm.
That is not a contradiction.
Recommended ranges are starting points. Actual hard-turning conditions should be adjusted according to the part, hardness, allowance, required finish, and machine condition.
The feed rate for this customer job was not included in the available process record, so we do not estimate or add one here.
This is important when reporting machining cases: actual data should remain actual data.
Continuous and Interrupted Cutting Are Different Applications
A smooth outside-diameter finishing cut and a shaft with a keyway may have the same hardness, but the cutting edge experiences two very different conditions.
Continuous Turning
For a stable continuous cut, the priorities are commonly:
- wear resistance;
- dimensional stability;
- surface finish;
- and predictable flank wear.
A high-wear-resistance PCBN grade can therefore be an excellent choice.
Interrupted Turning
When the cutting edge repeatedly enters and exits the workpiece—for example at:
- keyways;
- cross holes;
- splines;
- oil grooves;
- or other interrupted surfaces—
the insert is exposed to repeated impact.
Fracture resistance becomes much more important.
This is why PCBN manufacturers offer tougher grades specifically for interrupted hardened-steel machining. Sumitomo’s current grade-selection system, for example, differentiates high-speed finishing grades from higher-fracture-resistance grades intended for interrupted turning.
The lesson is simple:
Do not use a finishing-oriented CBN grade for a severe interrupted cut simply because both workpieces have the same HRC.
Should You Use High-CBN or Low-CBN-Content Inserts?
CBN content is another factor that customers sometimes oversimplify.
More CBN does not automatically mean better performance in every hardened-steel application.
For fine continuous finishing of hardened steels, lower-CBN-content PCBN grades with a ceramic binder are widely used because they can provide an effective combination of wear behavior and surface-finish capability.
For applications with greater interruption or toughness demand, a different PCBN composition and edge preparation may be necessary.
The correct selection should consider:
- workpiece hardness;
- continuous or interrupted cut;
- surface-finish requirement;
- machining allowance;
- cutting speed;
- required edge strength;
- and acceptable failure mode.
In other words, CBN percentage is only one part of grade selection.
Edge Preparation Matters More Than Many Users Expect
A PCBN cutting edge is rarely selected by substrate grade alone.
Chamfer and hone geometry can strongly influence edge strength.
A sharper edge can reduce cutting forces and help with fine finishing, but it may also be more vulnerable to chipping.
A stronger chamfered or honed edge improves security under higher load or interruption, but it can increase cutting forces.
This is particularly important with:
- keyways;
- holes;
- uneven stock;
- hardened scale;
- or varying depth of cut.
If a CBN insert is chipping early, changing the substrate is not always the first solution.
The first questions should include:
Is the edge preparation suitable for the cut?
and:
Is the cutting edge being overloaded on entry?
Should CBN Be Run Dry or With Coolant?
There is no universal rule that PCBN must always run dry.
Dry hard turning is very common because CBN can tolerate high cutting temperatures, and eliminating coolant can simplify the process.
Sandvik lists the possibility of eliminating coolant as one of the advantages of hard-part turning.
However, the correct cooling strategy still depends on:
- the PCBN grade;
- continuous versus interrupted cutting;
- part dimensional requirements;
- cutting parameters;
- and how consistently coolant reaches the cutting zone.
The key concern in interrupted hard turning is thermal cycling. Repeated heating and cooling can increase thermal shock at the cutting edge.
Therefore, an inconsistent cooling condition can be worse than a deliberately dry process.
The practical rule is:
Choose one controlled machining strategy and validate it. Do not allow coolant delivery to become intermittent or unpredictable at the cutting edge.
Can CBN Hard Turning Replace Grinding?
In some applications, yes.
One of the major reasons manufacturers use PCBN hard turning is that a hardened component can sometimes be machined directly to its final or near-final dimensional and surface requirements.
Hard turning can offer:
- shorter process routes;
- fewer setups;
- greater flexibility;
- easier machining of complex geometries;
- and reduced dependence on grinding.
Sandvik lists reduced production time, flexibility, and high component quality among the reasons for using hard-part turning.
Academic studies have likewise investigated hard turning as an alternative to grinding, and very low surface roughness has been demonstrated under appropriate PCBN machining conditions.
But it is important not to claim that CBN turning can replace grinding in every application.
Whether grinding can be removed depends on more than Ra.
You must also consider:
- roundness;
- cylindricity;
- dimensional tolerance;
- surface integrity;
- residual stress;
- subsurface thermal effects;
- and the functional requirement of the component.
Therefore, the technically correct statement is:
PCBN hard turning can replace or reduce grinding in suitable applications.
Why an Expensive CBN Insert Can Still Reduce Cost per Part
PCBN inserts usually cost much more per cutting edge than carbide.
That leads to a common purchasing mistake:
comparing insert price instead of machining cost.
Imagine two tools:
- Tool A costs less per insert but requires frequent indexing.
- Tool B costs more but runs much longer and holds size more consistently.
The cheaper insert may produce the more expensive component.
A more useful calculation is:
Tool cost per part = usable cutting-edge cost ÷ acceptable parts produced per edge
But even that is not the complete cost.
A real production comparison should also include:
- tool-change downtime;
- operator intervention;
- offset adjustment;
- dimensional inspection;
- rejected components;
- cycle time;
- machine utilization;
- and any grinding operation that can be reduced or eliminated.
This is why CBN should be evaluated at the process level, not simply at the insert-price level.
For a high-volume hardened shaft application, saving several tool changes per shift may be more valuable than the price difference between two inserts.
When PCBN Is NOT the Best Choice for 1045 Steel
CBN is an excellent tool material, but it is not always the right tool.
1. The 1045 Steel Is Still Soft
If the workpiece is annealed, normalized, or otherwise relatively soft, carbide is normally the first choice.
Using PCBN simply because it is a premium cutting-tool material usually does not make economic sense.
This is consistent with commercial PCBN application guidance. Kennametal, for example, specifically states not to apply its hardened-steel KB1610 PCBN grade to soft steel.
2. The Setup Is Unstable
If the machine or workpiece is vibrating, solve the rigidity problem first.
A more expensive insert will not eliminate chatter caused by:
- excessive overhang;
- poor workholding;
- loose components;
- or insufficient machine rigidity.
3. The Cut Is Severely Interrupted
PCBN may still be suitable, but the grade and edge preparation must be selected specifically for fracture resistance.
A fine-finishing PCBN grade may chip quickly in the wrong interrupted application.
4. The Machining Allowance Is Excessive or Highly Variable
A finishing-oriented CBN edge should not be forced to absorb unexpectedly large stock variation.
Where possible, stabilize the allowance before the final hard-turning pass.
5. Production Volume Is Very Low
For a one-off part or very low-volume job, carbide or another tool material may remain more economical even if PCBN could technically perform better.
The correct choice is the one with the lowest practical cost for the production requirement—not necessarily the longest theoretical tool life.
Troubleshooting PCBN Turning of Hardened 1045 Steel
When a CBN application does not perform as expected, changing the CBN grade immediately is often the wrong first move.
Problem: Surface Finish Is Poor From the First Part
Check:
- feed rate;
- nose radius;
- wiper geometry;
- runout;
- machine rigidity;
- workpiece clamping;
- and vibration.
Problem: Finish Is Good Initially but Gradually Deteriorates
Check:
- flank wear;
- notch wear;
- tool-change criterion;
- dimensional drift;
- and whether the insert is being used too long.
Problem: The Edge Chips Suddenly
Check:
- interrupted sections;
- machining allowance variation;
- edge chamfer or hone;
- feed and depth of cut;
- entry conditions;
- workpiece scale;
- and coolant delivery.
Problem: Tool Life Is Much Shorter Than Expected
First confirm:
- actual workpiece hardness;
- actual cutting speed;
- PCBN grade;
- continuous versus interrupted cutting;
- machine rigidity;
- and whether the selected insert is intended for that type of hard turning.
Do not assume that every short-tool-life problem is caused by “poor CBN quality.”
Often, the actual cause is a mismatch between the insert and the application.
A Practical Process for Setting Up a New CBN Hard-Turning Job
For a new hardened-steel application, we recommend the following approach:
- Confirm actual hardness. Do not select the insert based only on “1045 steel.”
- Identify whether the cut is continuous or interrupted.
- Check machining allowance and stock consistency.
- Choose a PCBN grade and edge preparation for the actual cutting condition.
- Start with conservative parameters.
- For continuous hardened-steel turning, begin around the lower end of Vc 120–180 m/min, f 0.10–0.12 mm/rev, and ap 0.10–0.30 mm where appropriate.
- Inspect the edge after the first test cuts.
- Check surface finish and dimensional stability.
- If the process is stable, increase cutting speed gradually.
- Judge the final condition by cost per acceptable part, not cutting speed alone.
This method is usually more reliable than starting with aggressive parameters and trying to solve edge failure afterward.
Frequently Asked Questions
Can CBN machine AISI 1045 steel?
Yes, especially when AISI 1045 has been hardened. For soft or normalized 1045 steel, carbide is usually the more economical first choice.
At what hardness should I consider PCBN?
There is no single mandatory transition point. Commercial PCBN grades are commonly available for hardened steels above approximately 45 HRC, while many conventional hard-part turning applications are in the 50–60+ HRC range.
Can CBN turn 1045 steel at HRC 58–60?
Yes. We have a customer application running a hardened-steel workpiece at HRC 58–60, with Vc 120 m/min and ap 0.08–0.10 mm.
The specific workpiece grade is not identified in the available customer process record, so this example should be viewed as a real reference for the hardness and cutting condition rather than as proof of an AISI 1045-specific result.
What cutting speed should I start with?
For continuous CBN turning of hardened steel, our practical starting range is:
Vc: 120–180 m/min
We recommend beginning at the lower end and increasing the speed after confirming cutting-edge stability and surface quality.
What feed do you recommend?
For continuous hardened-steel turning, a practical starting range is:
f: 0.10–0.12 mm/rev
Adjust according to surface-finish requirement, insert geometry, rigidity, and the CBN grade.
What depth of cut should I use?
Our normal starting recommendation is:
ap: 0.10–0.30 mm
For demanding finishing conditions or very high hardness, a lighter depth may be appropriate. One customer application at HRC58–60 is running at approximately 0.08–0.10 mm.
What surface finish can CBN achieve?
Sub-micron Ra is possible with a stable PCBN hard-turning process.
A practical target of approximately Ra 0.4–0.8 μm may be achievable in suitable finishing conditions, but the result depends strongly on feed, nose geometry, machine rigidity, tool wear, and the workpiece itself.
It should not be treated as a guaranteed value without a machining test.
Does CBN last 10 times longer than carbide?
It can in some applications, but there is no universal 10× rule.
Tool life must be compared under the same hardness, cutting condition, production requirement, and failure criterion.
The most useful measurement is acceptable parts per edge and cost per finished part.
Should CBN be used dry?
Dry hard turning is common, but it is not an absolute rule.
The correct choice depends on the PCBN grade, cutting condition, continuous or interrupted machining, and coolant stability.
Can CBN hard turning replace grinding?
In suitable applications, yes.
However, the decision should consider dimensional tolerance, geometry, surface integrity, and functional requirements—not surface roughness alone.
Conclusion
The most important question in machining hardened AISI 1045 is not:
“Can CBN cut 1045 steel?”
It can.
The better question is:
“At this hardness, with this machining condition and this production requirement, is PCBN the most stable and economical choice?”
For relatively soft 1045 steel, carbide is normally the logical solution.
As hardness increases into the hard-turning range, PCBN becomes increasingly attractive because of its wear resistance, dimensional stability, and ability to maintain a fine surface finish.
For continuous hardened-steel turning, our practical starting range is:
Cutting speed: 120–180 m/min
Feed: 0.10–0.12 mm/rev
Depth of cut: 0.10–0.30 mm
But these are starting values—not fixed rules.
Start conservatively. Check the cutting edge. Check the surface finish. Confirm dimensional stability. Then increase cutting speed gradually.
And when comparing PCBN with carbide, do not compare only the price of the inserts.
Compare:
tool life, machine downtime, surface consistency, operator intervention, and cost per acceptable part.
That is where the real value of PCBN hard turning becomes clear.
Need Help Selecting CBN Parameters for Your Application?
If you are machining hardened 1045, C45, S45C, bearing steel, tool steel, or another hardened ferrous material, the most useful information to provide is:
material grade, hardness, continuous or interrupted cut, workpiece diameter, machining allowance, required surface finish, and current cutting parameters.
With those details, the CBN grade and starting parameters can be selected much more accurately than by material name alone.